In this article
- III Electrode Metal Suggestions
- APPENDIX
- Welding Austenitic Stainless Steel Sheet, Plate and Pipe by SMAW Process
- 1. Scope
- 2. References
- American Petroleum Institute (API)
- 650 Welded Steel Tanks for Oil Storage
- American Society for Mechanical Engineers (ASME)
- B 31.3 Process Piping
- Section IX Welding and Brazing Qualifications
- 3. General
- 4. Safety
- 5. Materials
- 6. Procedure Format
- 7. Inspection
- American Iron and Steel Institute
- American Society for Testing and Materials
- SCOPE
- REFERENCES
- GENERAL
- SAFETY
- MATERIALS
- PROCEDURE FORMAT
- INSPECTION
TABLE
I Information Summary for Stainless Steel Pipe Welds Made in the Vertical Position (6G)
II Information Summary for Stainless Steel Plate Welds Made in the Vertical Position (3G)
III Electrode Metal Suggestions
APPENDIX
A Single Vee QW-482 Format for Welding Procedure Specification (WPS)
B Single Vee QW-483 Format for Procedure Qualification Record (PQR)
Welding Austenitic Stainless Steel Sheet, Plate and Pipe by SMAW Process
1. Scope
This Article is about welding austenitic stainless steel 1.6-20 mm (1/16-3/4 in) thick sheet, plate, and pipe in all positions by Shielded Metal Arc Welding (SMAW) process.
2. References
Reference is made in this standard to the following documents.
American Petroleum Institute (API)
620 Design and Construction of Large, Welded, Low-pressure Storage Tanks
650 Welded Steel Tanks for Oil Storage
American Society for Mechanical Engineers (ASME)
B 31.3 Process Piping
Section IX Welding and Brazing Qualifications
3. General
3.1 Where code welding is specified or required by the jurisdiction, qualification of both the procedure and individual welders as per ASME Section IX, shall be mandatory.
3.2 All tacks and new starts on root pass shall be feathered on all full penetration welds.
3.3 The GTAW process as per SES W06-F03 shall be used on austenitic stainless steel material whose thickness is less than 4 mm (5/32 in) and when ASME B 31.3 is specified. SES W13-F01 shall be used in other cases.
3.4 Adherence to applicable codes shall be mandatory. For ASME Code-approved work the shop shall be ASME authorized, and the procedure, as outlined on ASME forms on pages 7 through 10, shall be qualified for Code inspector’s approval at each site where it is to be used. Each welder doing ASME Code work shall also qualify for the inspector’s approval using the qualified procedure. The welder shall be a regular employee of that ASME authorized shop. For details refer to SES W11-F01.
3.5 Departures from this standard, for work not requiring ASME Code rules, may be practiced as long as testing and inspection are adequate to prove that weld quality is not impaired. For instance, ASME Section IX is referenced by ASME B 31.3 and API 620 and 650.
3.6 A sample of a qualified procedure is included. The information contained in this sample may be useful in qualifying your own welding procedure.
4. Safety
Safe practices prescribed in SES W02-F01 shall be followed on plant sites.
5. Materials
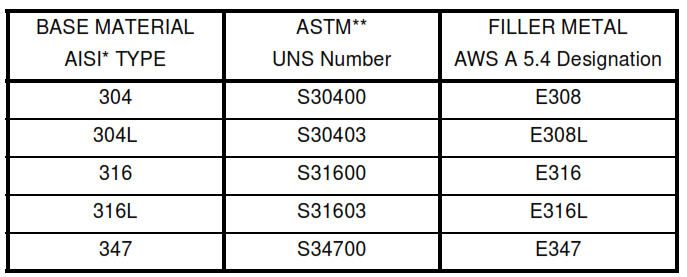
Materials for welding shall be as listed in Tables I, II, and III.
6. Procedure Format
6.1 Single Vee. QW-482 Format for Welding Procedure Specification (WPS). See Appendix A.
6.2 Single Vee. QW-483 Format for Procedure Qualification Record (PQR). See Appendix.
7. Inspection
7.1 The amount and type of inspection required depends on the service conditions and hazards to personnel and property. It is the responsibility of the originator to define the inspection requirements. Inspection shall be in accordance with applicable code(s).
TABLE I – Information Summary for Stainless Steel Pipe Welds Made in the Vertical Position (6G)

TABLE II – Information Summary for Stainless Steel Plate Welds Made in the Vertical Position (3G)
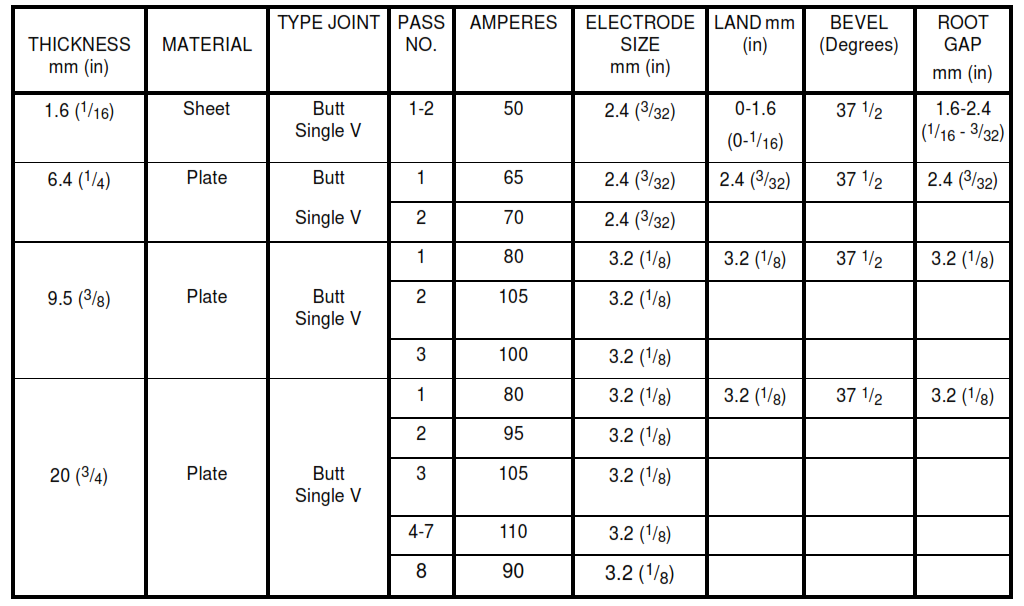
TABLE III – Electrode Metal Suggestions
American Iron and Steel Institute
American Society for Testing and Materials
Check following documents for appendices.
Discover more from PAKTECHPOINT
Subscribe to get the latest posts sent to your email.